
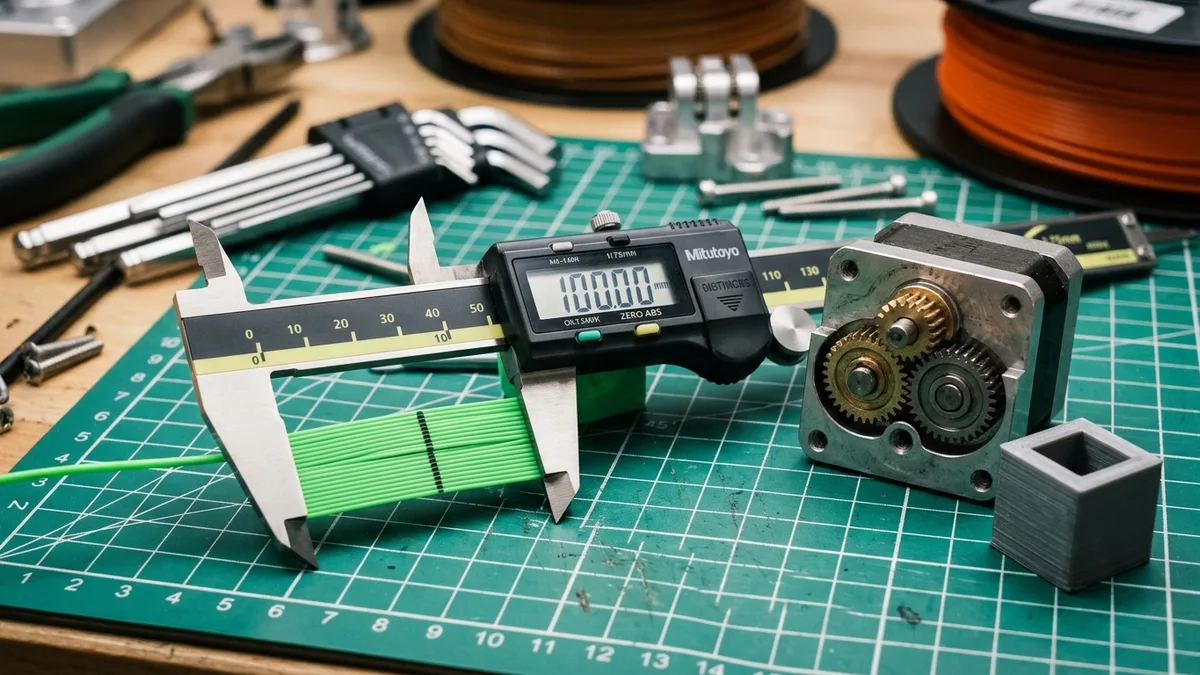
To design for 3D printing successfully, you must adjust minimum wall thickness, hole tolerances, overhang angles, and bridging lengths to match FDM limits. This guide covers how to design solid walls, achieve precise holes, print steep overhangs, span long bridges without supports, and prepare filament.
The Foundation: Minimum Wall Thickness
A wall in your 3D model must be a multiple of your nozzle diameter to ensure strength and print quality.
The Rule of Multiples
Your printer’s nozzle has a fixed diameter, typically 0.4mm. Your slicer creates walls by tracing the perimeter of your model with lines of extruded plastic, called perimeters or wall lines.
For a strong, solid wall, its thickness must be a multiple of your nozzle diameter.
- Bad Design: A 1.0mm thick wall. With a 0.4mm nozzle, the slicer can fit two perimeters (0.4mm + 0.4mm = 0.8mm), leaving a 0.2mm gap. It will try to fill this tiny gap with a shaky, weak line of infill, resulting in a fragile part.
- Good Design: A 1.2mm thick wall. This is a perfect multiple of a 0.4mm nozzle (0.4mm x 3 = 1.2mm). The slicer will lay down three solid, perfectly bonded perimeters.
Actionable Advice: For a standard 0.4mm nozzle, design your walls with these thicknesses:
- 0.8mm (2 perimeters): Good for most non-structural parts, like decorative models.
- 1.2mm (3 perimeters): Excellent baseline for functional parts that need to be handled, like brackets or enclosures.
- 1.6mm (4 perimeters): For parts that need to be genuinely strong and withstand mechanical stress.
Anything less than two perimeters (0.8mm) is asking for trouble. The part will be flimsy and you might see the infill pattern showing through the thin skin.
Precision and Fit: Designing Holes
Getting holes right is the difference between a functional part and a piece of scrap. Plastic shrinks as it cools, and the geometry of the printing process itself introduces errors.
Vertical vs. Horizontal Holes
- Vertical Holes: These are holes printed perpendicular to the build plate. They tend to print smaller than designed due to filament shrinkage.
- Horizontal Holes: These are holes printed parallel to the build plate. The top surfaces of the hole are essentially small bridges that tend to sag, resulting in an oval or egg-shaped hole instead of a perfect circle.
Actionable Advice for Vertical Holes: Grab your digital calipers. This is non-negotiable. To get an accurate fit, you need to add tolerance.
- For a loose fit (e.g., a pin that drops through), add 0.4mm to the hole diameter.
- For a snug fit (e.g., a bolt that threads in), add 0.2mm to the hole diameter.
So, for an M3 bolt (which has a 3mm diameter) to pass through easily, design the hole in your CAD model to be 3.3mm or 3.4mm. Print a small test piece first before committing to a 12-hour print.
Actionable Advice for Horizontal Holes: You have two great options to combat the sag:
- Design a Teardrop Shape: Instead of a perfect circle, modify the top of the hole into a 45-degree angle. This turns the bridging problem into a simple overhang problem, which the printer can handle easily. The bottom of the hole remains a true semicircle for accurate seating of a screw or bolt.
- Use Your Slicer: Modern slicers like PrusaSlicer and OrcaSlicer have a setting called “Hole Horizontal Expansion” or similar. This lets you add a specific offset (e.g., 0.15mm) to compensate for the sag without changing your CAD model.
Defying Gravity: Overhangs and The 45-Degree Rule
An overhang is any part of your model that extends outward, with no direct support below it. The printer creates an overhang by laying down a new layer that is only partially resting on the layer beneath it.
The golden rule is the 45-Degree Rule.
Most 3D printers can print overhangs up to a 45-degree angle from the vertical axis without any issues. At this angle, each new line of filament is supported by about 50% of the width of the line below it. It’s a safe, reliable limit.
Pushing Past 45 Degrees: You can print steeper angles, but you need to help your printer.
- Part Cooling is King: The faster you can solidify the extruded plastic, the less it will droop. A powerful part cooling fan is essential. Run it at 100% for overhangs.
- Slow Down: Reduce your print speed for overhang perimeters. Slicers have settings for this. A speed of 20-30 mm/s gives the fan more time to cool the filament.
- Lower Layer Height: A 0.12mm layer height will produce better overhangs than a 0.28mm layer height because each step outwards is smaller.
With good cooling and tuning, many modern printers can manage 60-degree overhangs. Anything beyond 70 degrees will likely fail and requires support structures.
Spanning the Gap: Mastering Bridges
A bridge is a section of a print that spans a horizontal gap between two points, with nothing but air underneath. Think of the top of a doorway. This is one of the most impressive FDM printing feats.
Success depends on stretching a line of hot filament taut and cooling it instantly so it freezes in place before it can sag.
Slicer Settings for Perfect Bridges:
- Bridge Speed: This is counterintuitive. Going too slow is bad; the filament has time to droop. Going too fast is also bad; the filament can snap or not anchor properly. A speed between 25-50 mm/s is a great starting point.
- Bridge Fan Speed: Set this to 100%. No exceptions. You need maximum cooling to solidify the filament strand mid-air.
- Bridge Flow/Extrusion Multiplier: Sometimes, reducing the flow for bridges to about 95-98% can help. This prevents a blob from forming at the start of the bridge and helps pull the line taut.
A printer with a rigid frame and precise motion system is critical for clean bridges. CoreXY printers are particularly good at this due to their lightweight printheads and stable mechanics.

Bambu Lab P1S Enclosed 3D Printer
Pros
- Fully enclosed CoreXY chassis with auxiliary cooling fan, Smooth multi-color / multi-material integration with Bambu AMS, Reliable out-of-the-box first layers with dual automated bed leveling, Active vibration compensation and belt tension monitoring
- Enclosure helps with temperature-sensitive materials like ABS and ASA.
- Excellent part cooling is ideal for aggressive overhangs and long bridges.
Cons
- Proprietary closed ecosystem
- Chamber is passively heated by the bed rather than a dedicated PTC heater
- Upgrading to hardened nozzle for carbon fiber requires separate swap
A machine like the Bambu Lab P1S excels at these challenges. Its powerful cooling and high-speed motion control make difficult geometry like steep overhangs and long bridges far more reliable.
The Non-Negotiable Input: Filament Quality
You can have the best printer and the perfect design, but if your filament is wet, your prints will fail. This is especially true for overhangs and bridges.
Filaments like PLA, PETG, TPU, and Nylon are hygroscopic. They absorb moisture from the air. When this wet filament enters the hotend (200°C+), the water inside instantly turns to steam and explodes out of the nozzle tip. You can hear it as a popping or crackling sound. This micro-explosion disrupts extrusion, causing:
- Weak, foamy filament that cannot span a bridge.
- Poor layer adhesion, causing overhangs to curl and delaminate.
- Excessive stringing and blobbing that ruins the surface finish.
Actionable Advice: Dry your filament. Do not assume a new roll from a sealed bag is dry. It often isn’t. An oven can work in a pinch (use the lowest temp, ~40-50°C for PLA), but it’s risky and inaccurate. A dedicated filament dryer is a simple, foolproof investment.
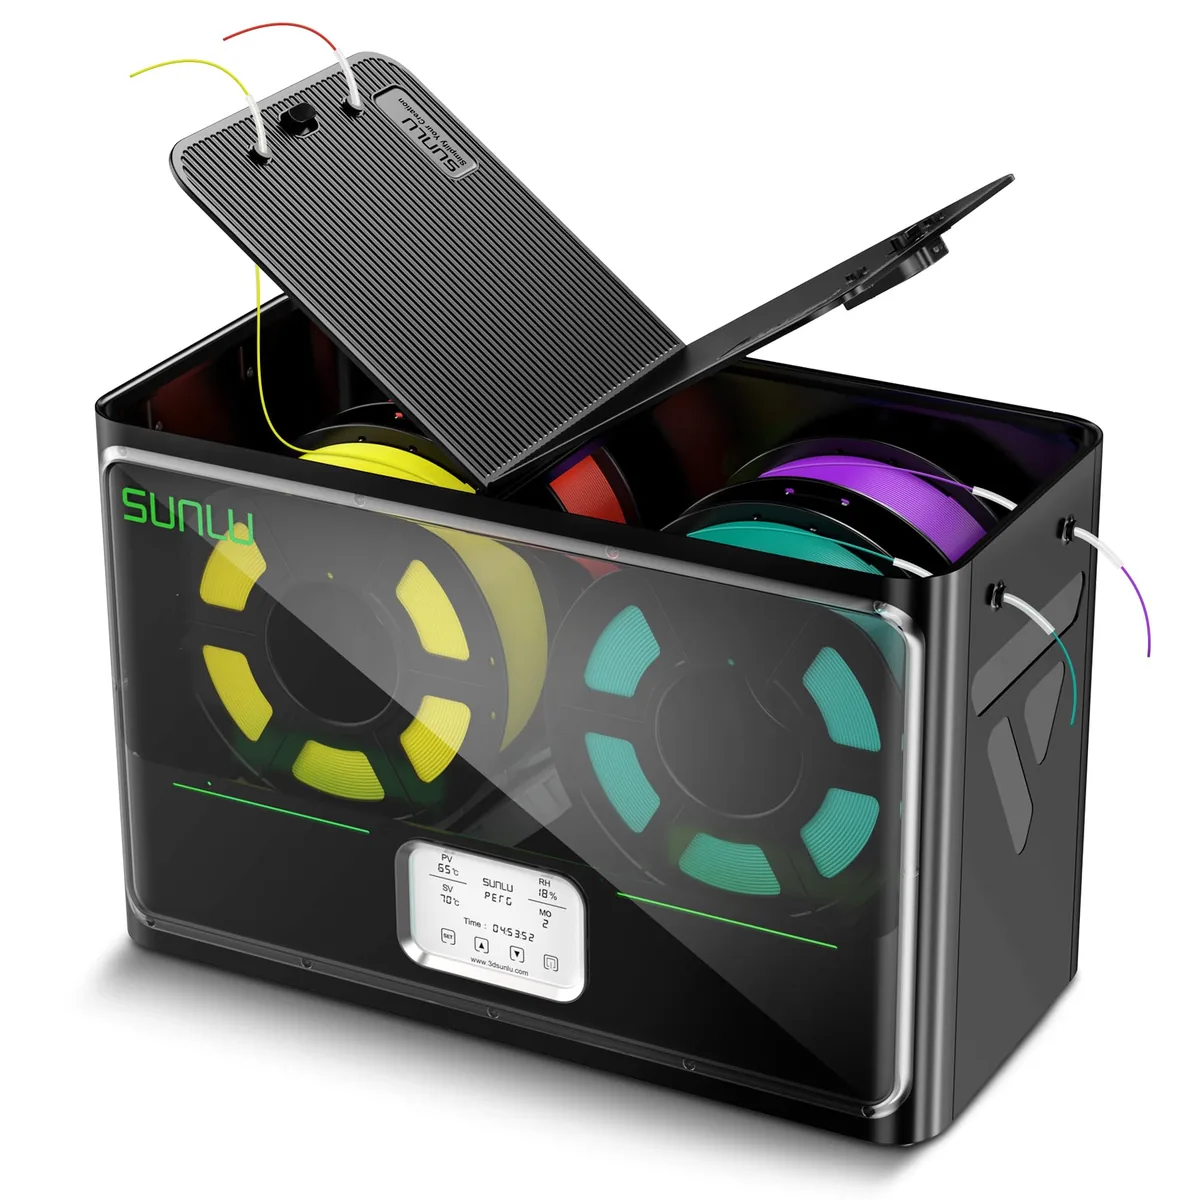
SUNLU S4 Pro 4-Spool Filament Dryer & Drybox
Pros
- Massive 4-spool capacity dries 4 rolls simultaneously for multi-color or multi-printer setups.
- 350W rapid PTC heating with three high-flow circulation fans up to 70°C.
- 8 dedicated filament feed ports with PTFE tubing allow direct printing while drying.
Cons
- Requires dedicated 515 x 267 x 268 mm desktop shelf space.
Investing in a multi-spool dryer like the SUNLU S4 Pro means you always have dry, ready-to-print material. Keeping your filament in top condition is a crucial part of routine 3D printer maintenance.
Design for Printing: A Summary Table
Use this table as a quick reference when you’re in your CAD software. These are guidelines for a typical 0.4mm nozzle setup.
| Feature / Parameter | Risky Zone (Likely to Fail) | Safe Zone (Calibrated Printer) | Aggressive (Expert Tuning) |
|---|---|---|---|
| Wall Thickness | < 0.8mm or non-multiples | 0.8mm, 1.2mm, 1.6mm | 0.4mm (for vase mode/flex) |
| Vertical Hole Ø | +0.0mm to +0.1mm | +0.2mm to +0.3mm | +0.15mm (dialed-in printer) |
| Overhang Angle | > 60° | 0 - 45° | 45° - 65° |
| Bridge Length | > 75mm | < 50mm | > 100mm (with perfect tuning) |
Test, Calibrate, and Repeat
Stop guessing. The 3D printing community has created countless calibration models designed specifically to test these features. Search on Printables or Thingiverse for “overhang test,” “bridge test,” or an all-in-one calibration model.
Print one of these models. Grab your calipers and measure the results.
- Did the 60-degree overhang start to curl? Your cooling might be insufficient, or you need to print slower.
- Did the 50mm bridge sag? Try increasing your bridge speed slightly or checking your filament for moisture.
- Did the 3mm hole print at 2.7mm? Now you know your printer’s specific tolerance and can adjust your designs accordingly.
Designing for 3D printing is not about finding a magic set of rules. It is an iterative process. You design, print, measure, and then refine your design or your slicer profile based on real-world results. By understanding these core geometric constraints, you can move from frustrating failures to reliable, functional parts. You can find more desktop 3D printing guides in our related tutorials.
How to Choose a Desktop 3D Printer
Finding a machine capable of handling strict tolerances and long bridges is crucial for structural parts. Learn what to look for in a 3D printer to ensure your hardware matches your design goals.
Desktop 3D Printer Comparison Chart
Evaluating project needs, material compatibility, and workspace limits leads directly to our Desktop 3D Printer Comparison Chart. For a comprehensive overview, review our 3D printer spec comparison.